For generations, a machine that had outlived its loan was a quiet point of pride on the factory floor. A press installed in the 1990s or a packaging line the crew knew well was often called a workhorse, and the usual plan was to keep it running as long as it made good output.
Today, however, the full cost of keeping that workhorse running is harder to ignore. Costs that once sat with the maintenance crew now appear in downtime reports, energy bills, audit findings, and data dashboards. Taken together, they can change the financial case for keeping an older machine in service.
Costs that land on different budgets
Older machines rarely send one large invoice. Repairs go to maintenance, lost output to production, extra power to utilities, and scrap to quality. Each department sees a slice, But the combined cost can remain difficult to track.
Unplanned downtime is often the largest piece. A 2024 Siemens report estimated that it costs the world’s 500 biggest companies about $1.4 trillion a year, or roughly 11 percent of revenue.
That number deserves some caution. Siemens sells predictive maintenance software, which may shape how the problem is framed, and the estimate covers every cause of downtime, not only equipment age. It also describes very large firms, so a mid-sized stamping plant could land well above or below that share.
Why the gap appears to be widening
Several pressures seem to be arriving together. Manufacturers eventually stop supporting older models, and plants may end up searching secondary markets for parts or paying a machine shop to make them. Longer parts searches and specialist repairs can also make breakdowns harder to resolve quickly.
Technical knowledge is a quieter risk. A technician nearing retirement may recognize a failing gearbox bearing by sound, yet that expertise may never have been documented. When experienced workers leave, plants can lose practical knowledge that helps them diagnose faults and avoid unnecessary downtime.
Energy adds a third layer. International Energy Agency (IEA) analysis has attributed roughly two-thirds of industrial electricity use to electric motors, and older motors and drives are often less efficient than current designs. How much that matters vary. A machine running two shifts on inexpensive power may take years to repay an upgrade, while one running around the clock under high tariffs may pay back sooner.
Letting old machines report in
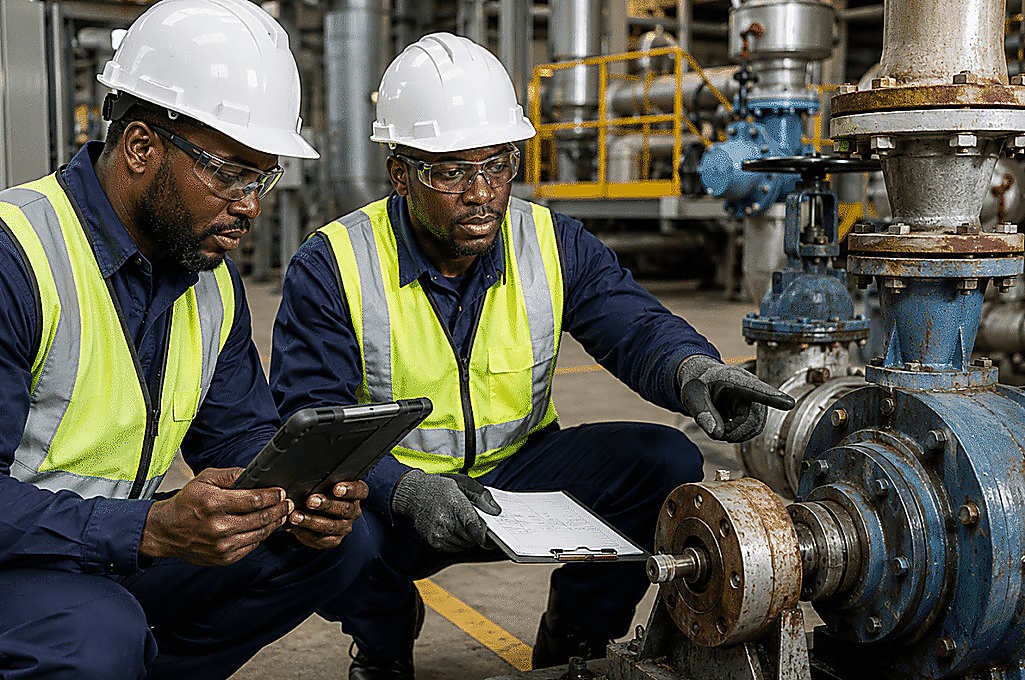
Condition monitoring is one way to close part of that gap without buying new equipment. Sensors that track vibration, temperature, or electrical current can give a rough warning before a component fails. For example, a plant might fit vibration sensors to a critical compressor. If the readings change, the repair can be scheduled for a planned weekend stop instead of an unplanned mid-week breakdown.
A 2010 U.S. Department of Energy guide estimated savings of 8% to 12% from preventive maintenance compared with preventive maintenance alone. That estimate provides a benchmark, not a guaranteed return for every factory. Actual results depend on equipment criticality, monitoring costs, the faults that can be detected and the plant’s response to alerts.
The approach has limits. It requires upfront spending and someone able to interpret the data, and some failures give almost no warning. Sensors can improve visibility into equipment condition, but they cannot eliminate mechanical wear or compensate for every maintenance weakness.
Retrofitting controls or safety systems can extend a machine’s life at a fraction of replacement cost. Yet upgrades cannot automatically resolve structural wear, deteriorating mechanical components or design limitations that have become operational constraints. The condition of the underlying machine still matters.
The same math does not fit every plant
A high-volume supplier with one line feeding an entire customer program faces different risk than a job shop with interchangeable machines. For the former, a breakdown may disrupt deliveries across an entire program. For the latter, production may be shifted to another machine, reducing the immediate impact.
Plants short on capital, or facing long delivery times for new equipment, can reasonably stretch asset life and upgrade in order of risk. Others, especially those under tighter safety or emissions rules, may find that replacement makes sense sooner.
Measures such as mean time between failures and maintenance cost per unit produced can show which situation applies. They still rest on forecasts of demand, energy prices, and downtime, and forecasts of that kind carry considerable uncertainty.
Even then, the decision depends on assumptions about future demand, energy prices and equipment reliability. A replacement that appears attractive under one set of forecasts may be harder to justify if production falls or the expected energy savings do not materialize.
Why the old machine may still win
Replacement is easy to describe as cleaner than it is. New equipment brings commissioning delays, a learning curve for operators, and occasional early-life failures. Older machines are often simpler, can be repaired with in-house skills, and are well known to the people who run them. Some perform specialized work that modern equivalents handle only at high cost.
Scheduled preventive maintenance also still works, particularly where crews know their equipment well. Its weakness is that fixed intervals can miss a failure that develops between inspections or replace parts that still had life left.
Reading the full ledger
What seems to be changing is visibility. Costs once scattered across departments are easier to measure, which gives plants a firmer basis for choosing among repair, retrofit, and replacement. What holds is the logic that made the workhorse attractive: dependable output from an asset already paid for.
Whether that logic still applies depends on the machine, the plant, and the customers it serves. The workhorse still earns its place in many factories. It simply helps to know what it costs to feed.